High-volume cutoff is a different problem from job-shop cutting. At 8,000–50,000+ cuts per shift, the machine is no longer a saw — it is a process station whose uptime, index accuracy, and blade-change downtime decide the throughput of the entire line. This guide walks the variables that actually move the needle, with the numbers buyers should put in a spec sheet.
Before comparing models, fix the production target. High-volume metal cutoff typically means:
| Volume tier | Cuts / shift | Duty | Expected CPM |
|---|---|---|---|
| Medium batch | 2,000–8,000 | 1–2 shift | 2–5 |
| High volume | 8,000–25,000 | 2–3 shift | 6–12 |
| Mass production | 25,000+ | 3 shift, automated | 12–25+ |
CPM (cuts per minute) is the metric that matters: CPM = 60 / (load + cut + unload + index + clamp). A fast spindle is worthless if indexing or clamping eats the cycle. When KEENSAW scopes a line, the index time and bundle-change time are weighted as heavily as the cutting speed.
Rigidity controls cut squareness and blade life at volume. Three families dominate:
| Frame | Rigidity | Best for | High-volume fit |
|---|---|---|---|
| Pivot (semi-auto) | Low | Low volumes, mixed sections | Poor — vibration shortens blade life |
| Column / twin-column | High | Continuous bar & tube | Strong — the KEENSAW default for lines |
| Portal / gantry | Very high | Large billets, heavy sections | Best for heavy mass production |
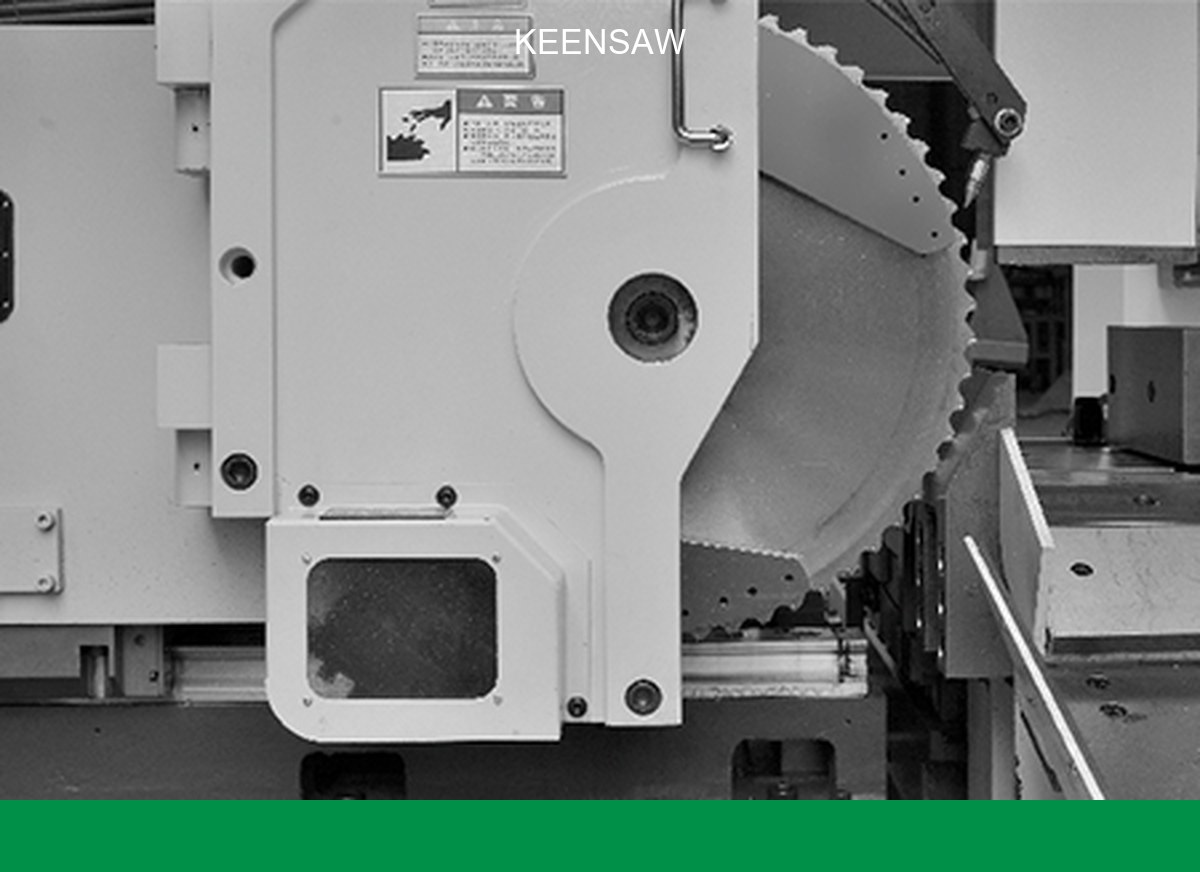
For sustained high-volume cutoff, choose a column or portal CNC circular saw — the stable frame keeps the kerf square and protects the expensive carbide blade from chatter. See KEENSAW’s Type A/B/C and pivot selection guide for the full family comparison.
The blade is the real consumable cost. The three production-grade options:
| Blade | Surface speed | Life (steel) | Cost / cut | Use case |
|---|---|---|---|---|
| HSS (high-speed steel) | Low–mid | Short | High | Low volume, soft alloys |
| TCT (carbide-tipped) | High | Long | Low | Steel, stainless, high-volume default |
| Cermet | Very high | Very long | Lowest | Mass production, thin-wall tube |
For most high-volume lines, TCT is the sweet spot: high surface speed for short cut times and long life that lowers cost-per-cut. KEENSAW’s high-speed CNC carbide circular saws and the KCS-160C automatic circular saw are built around TCT. For the blade-selection fundamentals, read the TCT saw blade guide.
Spindle speed is capped; index speed is not. The feed system decides CPM:
For continuous production, pair the saw with an automatic tube loader and separator so bundle change never stops the line.
Size the machine by the largest section it must cut at volume, not the average:
| Spec | What to check | Why it matters at volume |
|---|---|---|
| Round / square capacity | Max Ø and section mm | Must clear your 95th-percentile bar |
| Bundle capacity | Max bundle envelope | Bundle cutting multiplies CPM |
| Squareness tolerance | Typical <0.1 mm / 100 mm | Avoids downstream rework |
| Burr height | Target minimal | Reduces deburr station load |
KEENSAW’s carbide circular saws hold tight squareness because the rigid column frame resists deflection through the cut — the same reason CNC circular saws beat cold saws on repeatability at volume.
A worked example for Ø50 mm mild steel on a TCT CNC circular saw:
| Step | Time |
|---|---|
| Clamp + advance | ~1.5 s |
| Cut (TCT, high SFPM) | ~4–6 s |
| Retract + unload + index | ~1.5 s |
| Cycle | ~7–9 s → 6–8 CPM |
Then compute cost per cut = (blade cost ÷ cuts per blade) + (labor + power) ÷ CPM. This is where TCT wins: more cuts per blade at higher CPM. KEENSAW’s circular saw vs band saw TCO model and the band vs circular vs cold vs laser decision guide show the math across processes.
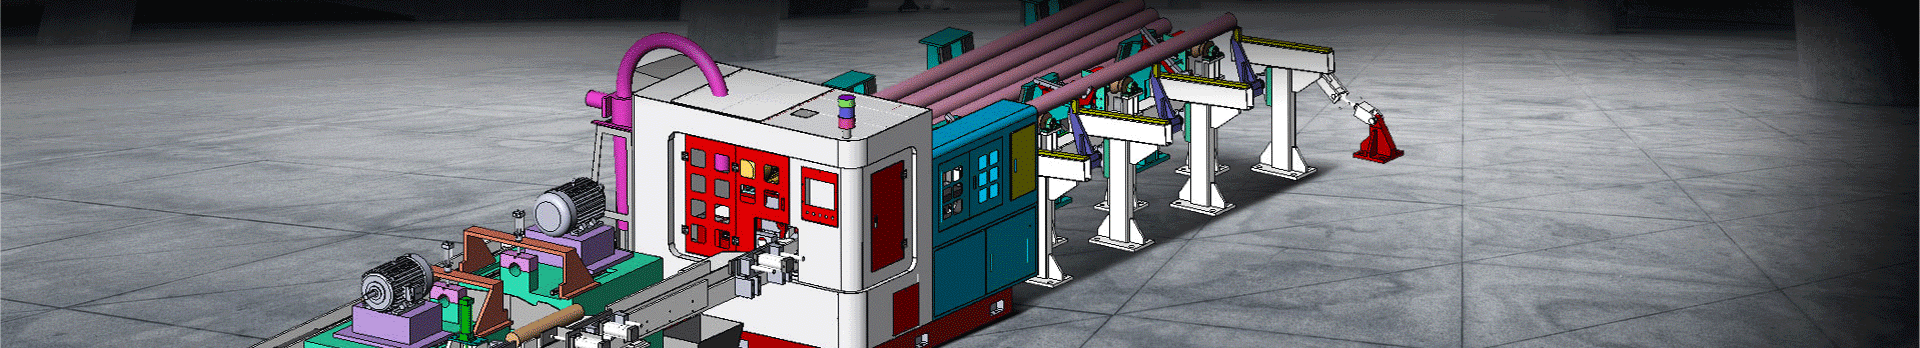
A saw is only as fast as its neighbors. A balanced high-volume cutoff line looks like:
Bundle decoiler / magazine → CNC circular saw → chamfer & deburr → discharge conveyor → MES/PLC.
Integrating cutoff with finishing is the single biggest throughput gain: KEENSAW’s automatic sawing-deburring lines double factory throughput by removing a handling step. Feed rates and blade parameters by material come from the cutting speeds & feeds reference.
For blade-level detail, see the circular saw blade buying guide.
For high-volume solids and heavy sections, a CNC circular saw wins on CPM, squareness, and burr. A band saw is better for very large or variable bundles where blade cost per cut on a single weird section matters more than speed.
Typically 6–12 CPM for Ø30–60 mm steel on TCT; cermet and smaller sections push higher. The limit is usually index + clamp time, not the spindle.
TCT for the broad default (steel, stainless, most sections). Cermet when you need maximum surface speed and blade life on thin-wall tube at very high volume — at a higher blade price.
Size to your 95th-percentile section (largest Ø or square you cut regularly) plus any bundle envelope, not the average bar. Undersizing is the most common line-stopping error.
Yes for repeats: cutting multiple bars in one stroke multiplies effective CPM and amortizes clamp time. It requires a machine rated for bundle envelope and a magazine feeder.
Contact us if you have any questions we will reply as soon aspossible