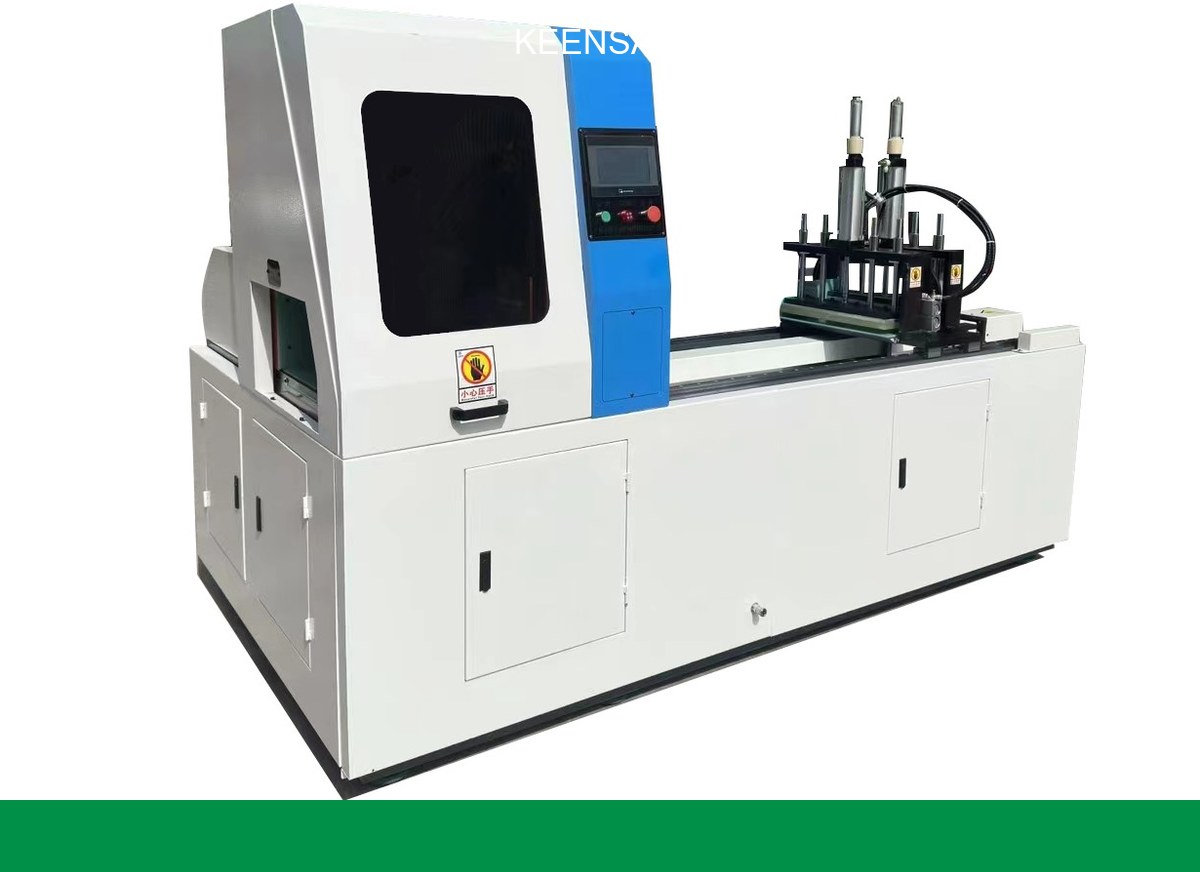
Short answer: The best aluminum cutting saw for burr-free extrusion profiles is a carbide-tipped, downward-cutting (pull/push) circular saw with a clamped, profiled fixture and flood or mist coolant, run at high RPM with a slow, steady feed. Burrs on extrusions come from the tooth exiting the thin wall, so the fix is geometry + clamping, not just a sharper blade: zero-clearance support at the cut, a negative/neutral rake carbide blade, and a vacuum or brush chip extraction that pulls swarf away from the profile.
Aluminum extrusions are thin-walled and asymmetric. When the saw tooth exits the far wall, the unsupported lip tears instead of shearing — that is the burr. The plate-vs-profile saw question matters because a saw tuned for thick plate will shred a thin-wall section.
| Element | Burr-free setting |
|---|---|
| Blade | Carbide TCG/negative-rake, 80–120 TPI region |
| Cut direction | Down-cut (push) so teeth compress, not lift |
| Clamping | Profiled/jaw fixture, zero clearance at cut |
| Speed | High RPM, slow steady feed (see RPM guide) |
| Coolant | Mist or flood; wax stick on thin wall |
| Extraction | Vacuum/brush pulls swarf off profile |
Aluminum wants high surface speed, but the machine’s RPM must match blade diameter — too slow and the tooth rubs (built-up edge, burr); too fast and the carbide chips. The KEENSAW aluminum-saw RPM guide gives the diameter-to-RPM table per alloy.


| Profile type | Key adjustment |
|---|---|
| Thin-wall (<2 mm) | Zero-clearance support + wax + slow feed |
| Thick-wall / solid | Standard carbide, higher feed OK |
| Anodized | Sharp blade, no coolant that stains |
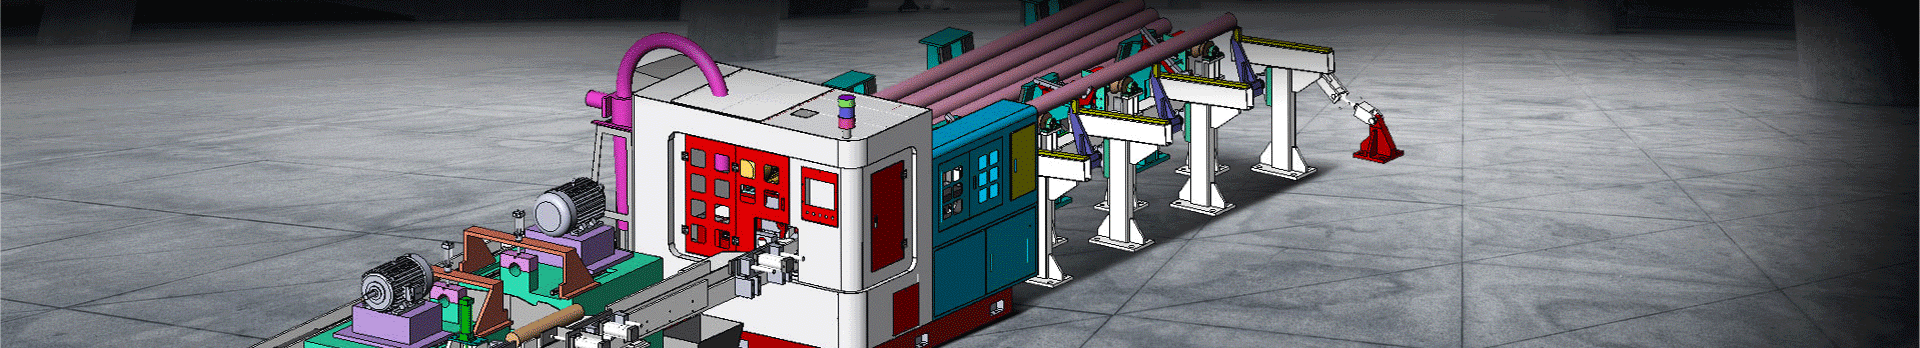
For continuous extrusion lines, an automatic aluminum cutting machine with servo feed and length stop delivers repeatable, burr-free cuts at volume. The aluminum saw selection guide walks the build-vs-buy decision.

Usually the tooth exits an unsupported thin wall. Add zero-clearance support at the cut and switch to a down-cut carbide blade.
High surface speed — match blade diameter to RPM per the RPM guide; too slow rubs and builds edge.
Carbide TCG for production; HSS only for occasional soft cuts.
Mist or light flood prevents built-up edge; for anodized, avoid coolant that stains — use a wax stick.
Different fixtures — see best saw for aluminum plate. A profile saw like the 505QA is purpose-built for extrusions.
Send the cross-section and wall thickness to the KEENSAW team for a burr-free setup sheet.
Share your extrusion cross-section, wall thickness, and target throughput — KEENSAW will specify the blade, RPM, clamping, and coolant combination that cuts your profile clean the first time. Request a quote →
Contact us if you have any questions we will reply as soon aspossible