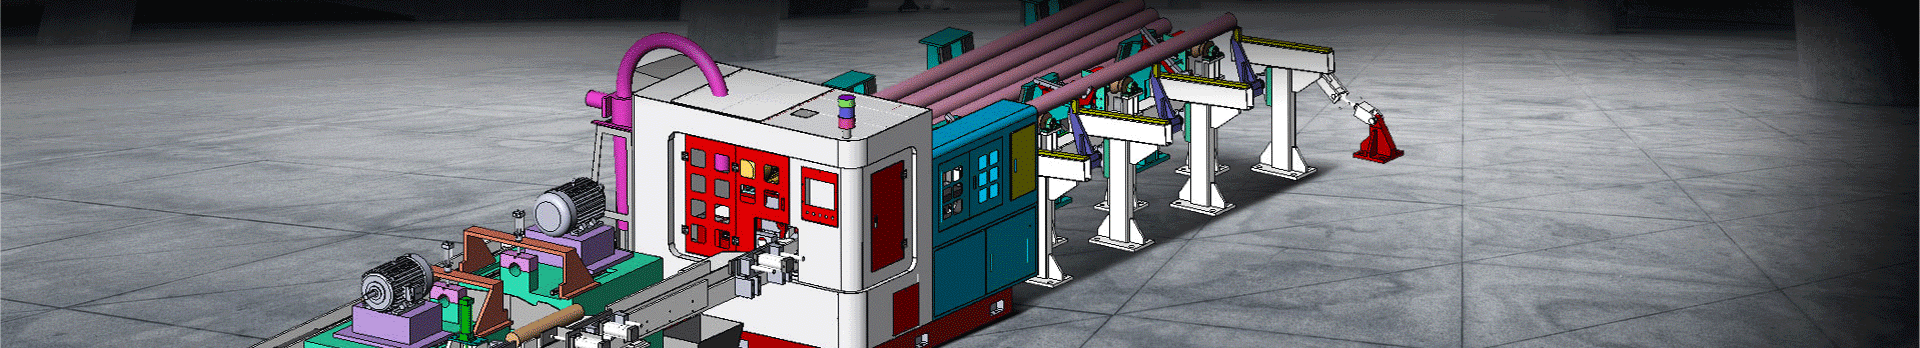
A band saw machine is a power saw that uses a long, continuous, toothed steel band stretched between two or more wheels to cut metal, wood, or composite stock. Unlike a circular saw that spins a rigid disc, the band saw’s blade runs in a closed loop at a controlled surface speed, which lets it make straight, curved, and miter cuts in very large sections without the heat and vibration a spinning disc generates. In metalworking shops the band saw is usually the first machine in the cutoff line—it rough-cuts bars, billets, tubes, and structural sections to length before any machining begins.
This guide goes further than a one-paragraph definition. We name every core component, explain how the blade actually removes metal, compare the main machine types, show how blade choice and capacity drive your result, and finish with a maintenance schedule and a buyer’s checklist you can take to a supplier. If you are specifying a machine for a new line, the capacity table and the FAQ at the end will save you a round of emails.
A band saw is defined by three things: a flexible endless blade, at least two wheels that carry it, and a worktable or vise that holds the stock. The blade is a thin ribbon of high-speed steel—usually bi-metal M42 or M51, sometimes carbide-tipped—with teeth on one edge. Because the blade is thin and the cut is a continuous scribing action rather than an intermittent chopping action, band saws remove material with very little power and produce a narrow kerf, so you waste less metal per cut.
What separates a band saw from a circular saw is not just blade shape. A circular saw bites with a few teeth at the bottom of the disc; a band saw presents a fresh tooth to the work on every pass of the loop. That even, continuous load is why a band saw stays smooth on a solid billet that would shake a circular saw apart, and why it can run unattended through a bundle of bars.
| Component | Function |
|---|---|
| Band wheels (drive + idler) | Carry and tension the blade; the drive wheel is powered by the motor through a gearbox. |
| Blade (bi-metal / carbide) | The cutting edge—tooth geometry sets the chip load, finish, and blade life. |
| Frame (column / gantry / scissor) | Rigid structure that resists deflection under cutting force; dual-column and gantry frames handle the largest sections. |
| Vise / clamp | Holds the stock rigidly so the cut stays square and safe; hydraulic or pneumatic, often with a movable jaw for bundles. |
| Blade guides & brushes | Support the blade near the cut and wipe away chips; worn guides cause wandering cuts. |
| Hydraulic / servo feed | Controls descent or feed rate—the biggest lever on blade life and cut quality. |
| Coolant system | Floods or mists the cut to control heat and flush chips (see our coolant guide). |
| PLC / HMI control | Stores cut length, piece count, feed pressure, and surface speed; on CNC machines it runs the whole cycle. |
| Chip conveyor / brush | Removes swarf so it does not pack the gullets or scratch the finished face. |
The blade is where the cut is won or lost. A band saw blade has a back (uncut top edge), a tooth tip, a gullet (the valley that clears the chip), and a set (the side offset that gives the kerf its width). Teeth-per-inch (TPI) controls chip load and finish: too few teeth and the cut chatters; too many and the gullets clog. Tooth form matters too—standard for general steel, hook for fast non-ferrous and soft material, skip for soft alloys and plastics where chip clearance is critical. We cover TPI in detail in our TPI chart guide.
Because the blade is a closed loop, every tooth re-enters the cut at the same speed. This even load is why band saws run smoothly on solid billets and why a single operator can tend several machines at once.
The blade arches over the stock and descends under gravity or hydraulics. This is the workhorse for cutting bars, tubes, and bundles to length. The 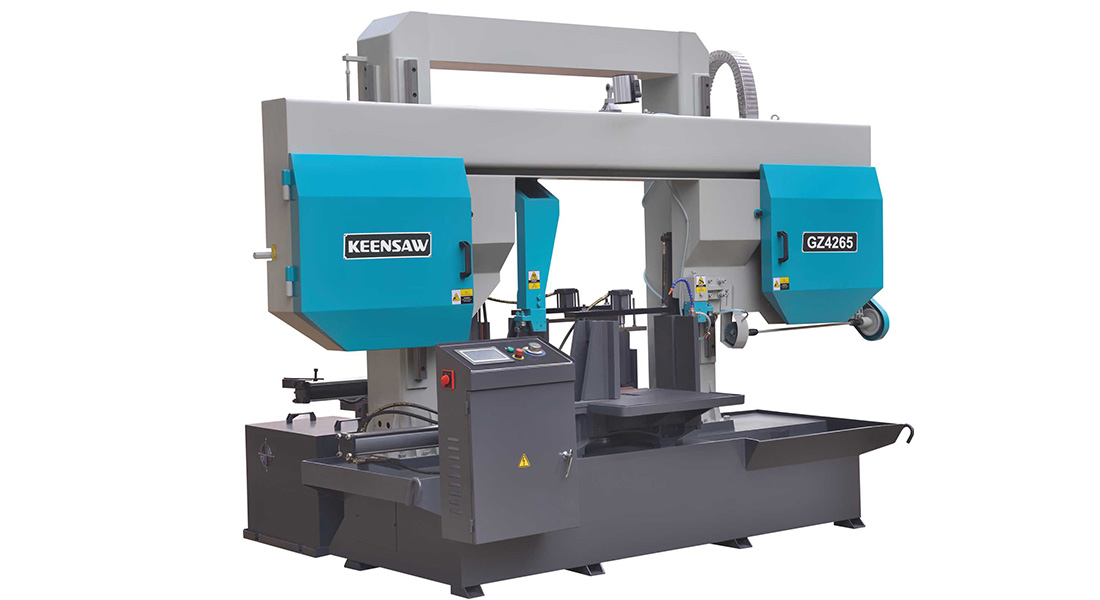 GZ4265 dual-column horizontal band saw is built for large billets and forging steel, while the BSVP530CNC targets high-speed automatic cutoff.
The table is horizontal and the blade runs vertically, so you can feed curved and internal contours. The 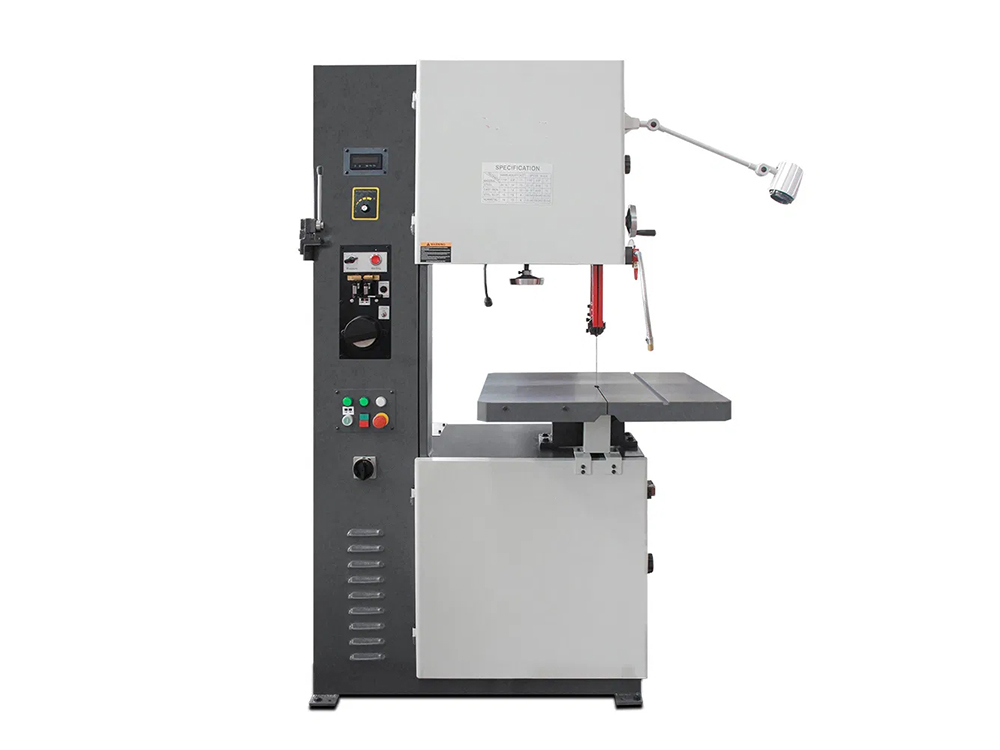 L-33/58S vertical band saw with tilting table and the G5350 are typical shop tools for contour and profile cutting.
These pivot the head or vise to cut angles without rotating the stock—ideal for structural steel and pipe joints. See the G4028Z60 and PX-35/65N NC miter band saw.
For structural sections and very large capacities, gantry and bundle machines cut multiple bars or wide flange sections in one pass. The G4252D bundle band saw and G42150 square-column gantry band saw are built for this duty.
| Method | Best for | Kerf | Heat affected zone | Typical use |
|---|---|---|---|---|
| Band saw | Large solid sections, bundles, contours | Narrow | Minimal | Rough cutoff, low cost/part |
| Circular / cold saw | High-precision, burr-free bar ends | Wider | None | Finish cutoff, weld-prep |
| Laser | Thin-wall tube, complex profiles | None | Localized | See our decision guide |
The machine is only half the story—the  bi-metal band saw blade sets your cut quality and blade life. M42 bi-metal covers most steels; M51 adds wear resistance for abrasive alloys; carbide-tipped blades handle stainless and high-strength grades at higher speed. Match TPI to the section thickness—read our TPI chart before ordering.
Band saws appear wherever stock must be cut to length before value is added: automotive and bearing plants (bar cutoff), aerospace (titanium and nickel alloy billets), construction (rebar and structural bundles), toolmaking (die steel), and fabrication shops (tube and pipe). The common thread is high volume at low cost per cut with minimal heat damage to the remaining bar.
| Machine type | Typical round capacity | Automation | Best duty |
|---|---|---|---|
| Manual / semi-auto horizontal | 180–330 mm | Manual feed | Jobbing, low volume |
| CNC horizontal (BSVP series) | 330–530 mm | Auto index, bundle | High-volume bar |
| Dual-column / gantry | 530–1,000+ mm | Auto index | Billets, forgings |
| Vertical contour | By table, not round | Manual / NC | Profiles, internal cuts |
| Miter / swivel | 250–650 mm | Manual / NC | Structural, pipe joints |
A band saw moves a sharp loop at speed. Minimum PPE is safety glasses and cut-resistant gloves for handling stock; hearing protection where the shop exceeds 85 dB. Keep guards closed, never reach across the blade path, lock out the machine before changing blades, and train operators on the emergency stop. Good housekeeping—clearing chips and managing coolant—prevents slips and Infections.
| Interval | Task |
|---|---|
| Daily | Check blade tension and tracking; top up coolant; clear chips. |
| Weekly | Inspect guides and brushes; verify vise squareness; check hydraulic oil level. |
| Monthly | Calibrate feed pressure; test emergency stop; clean tank and filter. |
| Per blade change | Clean wheels, confirm tracking, run in the new blade at reduced feed. |
Need help specifying a band saw for your line? KEENSAW builds horizontal, vertical, dual-column, gantry, and miter band saws from 180 mm to 1,000+ mm capacity. Contact our application team with your material, section size, and daily cut count—we’ll size the machine, blade, and coolant setup for you.
Contact us if you have any questions we will reply as soon aspossible