Short answer: A CNC tube bending machine beats a manual rotary bender on wall-uniformity, repeatability, and total cost of ownership the moment you run the same bend more than ~500×/month or need a cosmetic/structural tube. Manual benders win only for prototypes, one-offs, and low-mix shops. The ROI crossover is typically 8–14 months, because CNC eliminates scrap from inconsistent wall thinning, removes the skilled-operator bottleneck, and holds ±0.2 mm repeatability that manual bending cannot.
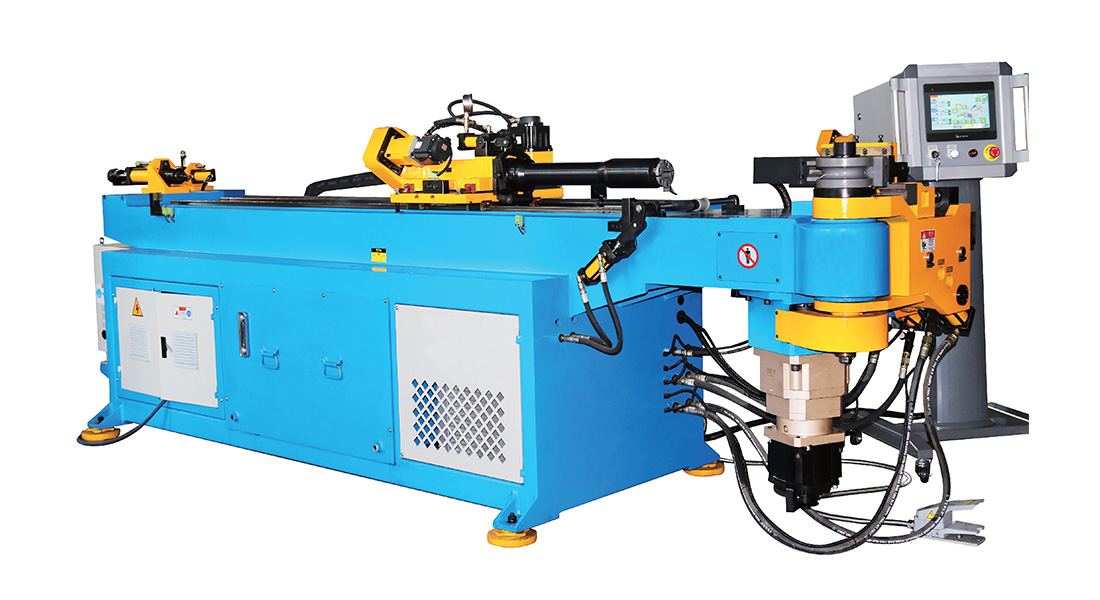
Manual rotary bending relies on the operator’s feel for speed, pressure, and mandrel position. That varies bend-to-bend, so wall thickness thins unevenly — a failure risk on pressure or structural tubes. A CNC bender drives every axis from a program, so wall thinning stays within spec every time. The mandrel bending 101 guide shows how axis control kills wrinkles and thinning.
| Factor | CNC tube bender | Manual rotary bender |
|---|---|---|
| Repeatability | ±0.2 mm | Operator-dependent |
| Wall uniformity | Held in spec | Varies |
| Setup / changeover | Recall program (seconds) | Re-jig by hand (minutes) |
| Operator skill needed | Low (load + unload) | High |
| Scrap rate | Low | Higher |
| Capital cost | Higher | Lower |
| Monthly volume | Lower cost/bend | Verdict |
|---|---|---|
| < 500 bends | Manual | Manual (prototype) |
| 500–2,000 bends | CNC (scrap savings) | CNC pays back ~8–14 mo |
| > 2,000 bends | CNC | CNC clearly |
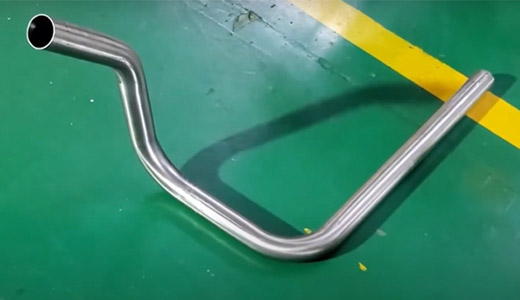
Not all CNC benders are equal. The CNC vs NC-hydraulic comparison and the CNC-or-NC buying guide help you choose axis count:
| Requirement | Choose |
|---|---|
| Tight radius + thin wall | CNC + mandrel + booster |
| Cosmetic exposed tube | CNC (no wrinkle) |
| Pressure/structural tube | CNC (wall in spec) |
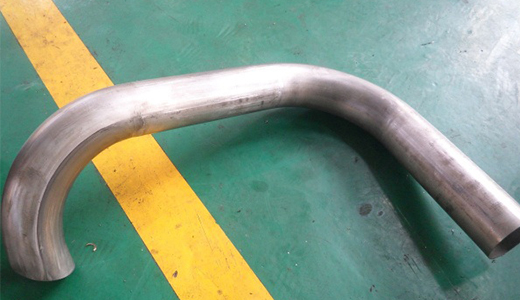
Around 500+ repeat bends/month, once you count scrap and operator time — payback is usually 8–14 months.
Yes. Programmed axis control keeps thinning within spec every bend; manual varies with operator feel.
See the full comparison; CNC electric for precision, NC hydraulic for budget programmatic bending.
A booster adds pressure for tight-radius thin-wall tube without wrinkling.
Only with skilled setup and a mandrel; consistency is the problem, not capability.
Send tube OD, wall, radius, and volume to the KEENSAW team for a configured quote.
Share your tube OD, wall, bend radius, and monthly volume — KEENSAW will model CNC vs manual ROI and wall-uniformity on your parts and recommend the right axis class. Request a quote →
Contact us if you have any questions we will reply as soon aspossible